Factory Audit & Supplier Scorecard for Jamnagar Brass Manufacturers
Highlights:
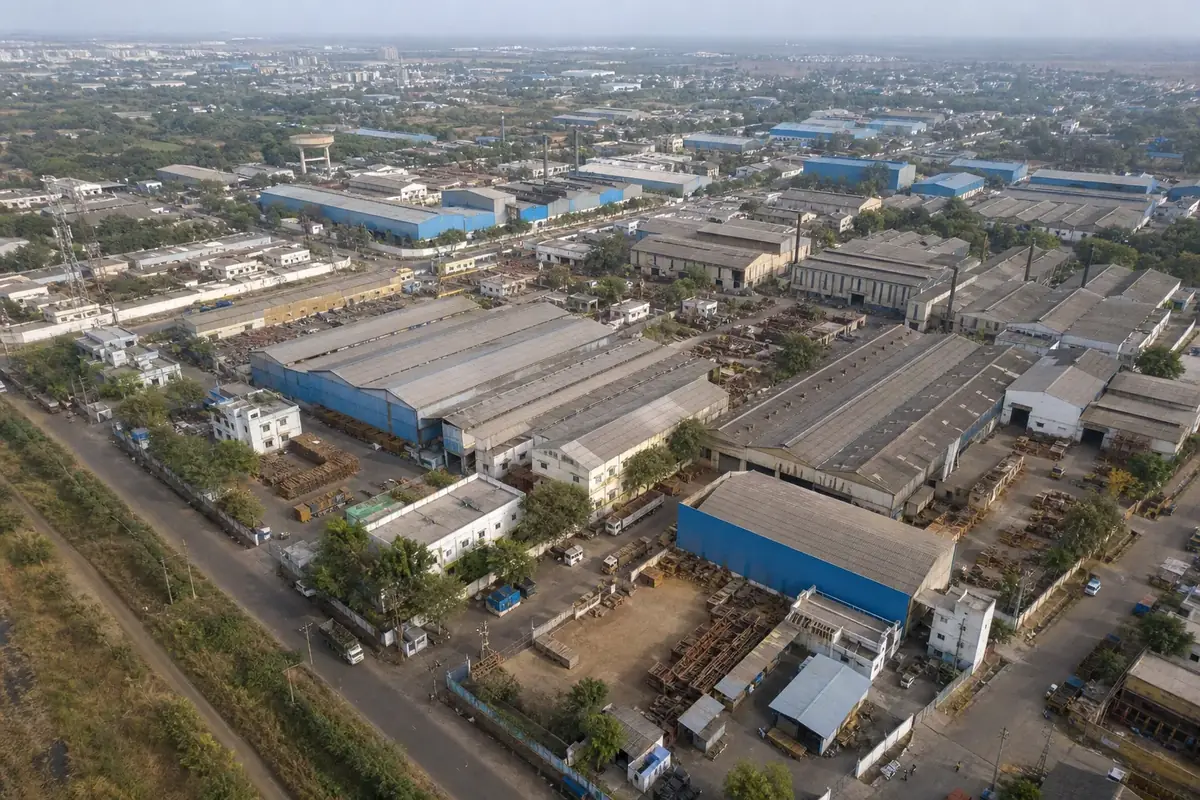
- Walk the GIDC shop floor—rod/extrusion incoming, cam versus Swiss CNC, plating, and packing—before you lock a supplier from a catalogue PDF.
- Score only in-house lab evidence: OES chemistry, calibrated Go/No-Go gauges, CMM programs, and ASTM B117 salt-spray records, not rented certificates.
- Write commercial terms into the PO: tooling ownership, sample-versus-production delta, MOQ, lead time, and Incoterms.
- Use a 100-point weighted scorecard; hold any vendor below 75 or with a lab score under 3/5, and kill the PO on documented red flags.
Related reading: pre-shipment quality inspection, engineering RFQ structure, and Jamnagar brass procurement.
1. Why a Factory Audit Beats a Catalogue Quote
A catalogue, a WhatsApp photo of a Swiss sliding-head, and a unit price on CW614N do not tell you whether that Jamnagar manufacturer can hold 6g threads after nickel, keep lead within drawing limits on the next melt, or ship the same process you approved at first article. Catalogue SKUs are often traded parts; your drawing is a process. The gap between those two is where dimensional drift, alloy substitution, and plating blistering enter the container.
Treat the audit as a go/no-go gate before tooling money and a production PO, not as a courtesy visit after the PI is signed. You are scoring four things a PDF cannot show: installed process (not borrowed machines next door), in-house metrology (not a rented spectro print), commercial control of tools and lots, and export packing that will survive Mundra-to-warehouse transit. Pair this audit with a drawing-complete engineering RFQ so the factory is quoting the process you will later score, not a generic brass insert.
Jamnagar’s strength is density of turning capacity across GIDC estates—not uniform process control. Two adjacent units can quote the same IS 319 Grade I rod and deliver different zinc, different cam wear, and different carton crush strength. The scorecard below exists so purchasing, quality, and engineering share one numeric decision instead of three conflicting impressions from a factory tour.
2. GIDC Shop-Floor Checks: Rod/Extrusion, Cam vs Swiss CNC, Plating, Packing
Walk the process in material-flow order. Do not start in the conference room. Ask to begin at incoming rod, then machines, then plating (in-house or named subcontractor), then packing. If the route is staged for you, note it—staged routes are a scoring penalty in Section 5.
Rod and extrusion incoming
Identify whether the unit extrudes in-house, buys rod from a named Jamnagar mill, or mixes both. Check heat-number tags on bundles, diameter and ovality on a sample bar, straightness (reject >0.5 mm/m for Swiss feed), and whether free-cutting versus forging rod is segregated. Ask which alloy grade is on the floor today versus what was quoted (C36000 / CW614N / CZ121 / IS 319). Photograph bundle tags; you will match them later to OES prints.
Cam automatic vs Swiss CNC
Count machines that are actually running your process family, not the installed nameplate. Cam autos (TRAUB / similar) are the right economics for high-volume, stable geometry; Swiss sliding-head (Tornos, Citizen, or equivalent) is the right process for long slender parts, deep holes, and tighter concentricity. Score a mismatch as a process risk: cam shops quoting Swiss-only tolerances, or a single Swiss cell hidden behind a cam-heavy floor. Check collet condition, bar-feed straightness, tool-offset discipline, and whether first-off and in-process checks are logged per spindle—not “we check sometimes.” Confirm the GIDC cluster capacity you are buying is in this shed, not a sister unit you did not walk.
Plating line or named subcontractor
If nickel, tin, or chrome is in-house, walk alkaline degrease, rinse, strike, and bath control charts (pH, temperature, amp-minutes). If plating is subcontracted, get the subcontractor name, distance, and whether incoming plated lots are XRF-checked before packing. Threaded parts must be cut for post-plate gauge pass; ask to see the undersize/oversize offset they use. A factory that cannot state micron targets (e.g. 5–8 µm Ni) is not process-capable on finish.
Export packing
Inspect inner cartons (typical 20–25 kg), VCI or oil film, silica gel, partition or polybag for plated parts, and ISPM-15 pallets. Crush a closed sample carton at the corner; weak flute plus overfill is a transit-scratch generator. Confirm heat/lot labels on master cartons match the rod tags you photographed at incoming. Packing is where traceability either survives the port or dies.
3. Quality Lab Evidence: OES, Gauges, CMM, Salt Spray vs Rented Certificates
Certificates are not a lab. Jamnagar units routinely attach EN 10204-style PDFs, ISO logos, and salt-spray reports generated by a rented instrument or a neighbouring shop. Your job is to see the equipment, the calibration stickers, the last three lots, and an operator who can run the method—not a laminated certificate on the wall. Use the same inspection logic you would apply at pre-shipment quality checks, but apply it to capability, not to a sealed carton.
Demand this evidence in the lab, on the day of the audit:
- Optical Emission Spectrometry (OES): See the spectrometer, argon supply, and spark stand. Ask them to spark a coupon from a tagged bundle you selected—not a prepared “demo” puck. Print must show Cu, Zn, Pb, Fe, and residuals with the heat number matching the bundle tag. Type 3.1 language without a matching heat is a Type 2.2 in costume.
- Thread and attribute gauges: Class 6g/6H Go/No-Go ring and plug gauges for the threads on your drawing, with calibration due dates. Worn shop gauges used as “production gauges” with a calibrated set locked in a cupboard scores as a fail on process control.
- CMM or optical measurement: For true-position, concentricity, and multi-feature first-article. Ask who wrote the last FAI program, whether it is stored, and whether it is re-run after tool change. A CMM used only when a buyer visits is not in-process control.
- Salt spray / coating thickness: ASTM B117 chamber in-house, or a named lab with your lot ID on the report. XRF or magnetic/eddy thickness on flats and thread roots. Hours-to-failure must be specified on the drawing (e.g. 24 / 48 / 96 h) or the report is theatre.
Rented-certificate tells: serial numbers that do not match the machine in the room; reports dated on Sundays; identical spectro tables reused across heats; a salt-spray photo with another company’s letterhead cropped; gauges with no ID. Any one of these drops the lab category to 1/5 and holds the PO regardless of price.
4. Commercial Terms: Tooling Ownership, Sample vs Production, MOQ, Lead Time, Incoterms
Process capability is wasted if the PO does not lock ownership, the sample-to-production delta, and the delivery term. Score these in writing; verbal “no problem” on a GIDC walk is not a term.
- Tooling ownership: Cam form tools, Swiss collets and guide bushings bought for your geometry, custom Go/No-Go gauges, and plating jigs paid by you are buyer property. Assign asset IDs, photo them, state storage location, and add a return-on-demand clause. Factory-standard inserts and worn collets are consumables. Do not bury tooling in a sample invoice with no title.
- Sample versus production: First-article from the production machine, production collet, production plating bath, and production packing—not a tool-room one-off. Require a written delta: if samples ran on Swiss and production will run on cam, that is a new PPAP, not a colour change. Freeze process on the FAI sign-off.
- MOQ: Separate sample MOQ, first production MOQ, and steady-state MOQ. Cam economics often need 5,000–10,000 pcs; Swiss can be lower. An MOQ that exists only to fill a melt or a plating barrel should be explicit so you can combine SKUs or accept a surcharge instead of a surprise quantity.
- Lead time: Split rod-on-hand versus rod-to-buy, plating queue, and packing. Ask what happens when the extrusion mill is down. A quoted 4 weeks that silently assumes rod in stock is a 7-week reality. Put a late-delivery remedy on the PI, not in an email thread.
- Incoterms: Name the term and the place (FOB Mundra, CIF destination port, EXW factory). EXW plus a factory-arranged trucker is not FOB. Confirm who insures, who files DGFT/ICEGATE documents, and who pays destuffing. Mismatched Incoterms are how brass lots sit in demurrage while two teams argue whose forwarder it is.
5. Weighted Supplier Scorecard for Jamnagar Brass Manufacturers
Score each category 1–5, multiply by the weight, and total to 100. Award a production PO only at 75 or above with no category below 3. A lab score of 1–2 is an automatic hold. Re-score after first article and after any ownership, machine, or plating-route change. Use the same sheet for every shortlisted GIDC unit so price is compared at equal risk.
| Category | Weight | 5 — Capable | 3 — Conditional | 1 — Fail / hold |
|---|---|---|---|---|
| Shop-floor process (rod/extrusion, cam vs Swiss, plating, packing) | 25% | Heat-tagged rod, process matches drawing (cam or Swiss), plating control or named sub with incoming XRF, export-grade packing | Process mostly fits; plating subcontracted without incoming check; packing adequate but labels weak | Staged tour, borrowed machines, mixed alloys on the floor, unknown plater |
| Quality lab (OES, gauges, CMM, salt spray) in-house | 25% | Live OES on your selected bar, calibrated 6g/6H gauges in use, CMM/FAI stored, salt-spray or XRF with lot ID | Equipment present; calibration overdue or methods not used in-process | Rented PDFs, serial mismatch, reused spectro tables — automatic hold |
| Commercial terms (tooling title, sample vs production, MOQ, lead time, Incoterms) | 20% | Buyer-titled tools with IDs, FAI on production process, split MOQ/lead time, named Incoterm + place | Terms agreed in email; tooling title not yet on PO | Verbal only; sample from a different process; EXW quoted as FOB |
| Traceability & export packing (heat numbers, carton/pallet) | 15% | Heat on rod, traveler, OES, and master carton; VCI/silica; ISPM-15 pallets | Lot tags exist but do not flow to carton; packing generic | No heat link; mixed lots in one carton |
| Remote-audit readiness & documentation | 15% | Unscripted video, live heat match, QMS records shareable, SGS/BV access allowed | Will video a prepared bay; documents slow | Refuses camera beyond office; blocks third-party inspection |
Scoring math: category points = (score 1–5) × weight × 20. Example: lab 4 × 0.25 × 20 = 20 points. Total 100. Record auditor, date, unit address, and machine counts on the same sheet so a later buyer can see what was actually walked.
6. Remote Audit: Live Video, Heat Numbers, SGS and Bureau Veritas
Use remote audit to shortlist, to re-qualify a scored vendor, or when travel is not possible before a limited first-article lot. Do not use it as the sole gate for a new high-volume or regulated part. Run it as a protocol, not a sales call.
Live, unscripted video: Buyer directs the camera. Start at the gate, then rod stores, machine bays (count spindles running), plating or dispatch-to-plater area, lab, packing. Refuse a pre-edited MP4. Timestamp and keep the recording with the scorecard.
Heat-number match on camera: Pick a bundle tag, then the OES print, then a packed carton. All three IDs must match in the same session. Screenshot each. A “we will email the certificate” after the call is a lab-category penalty.
Gauge and CMM on camera: Operator runs Go/No-Go on a part from the machine you are watching, then shows calibration labels. If a CMM exists, open the last FAI program—not a blank bed.
SGS / Bureau Veritas (and equivalent): Escalate to a paid third-party when lot value, PPAP, or drinking-water / electrical-safety rules require an independent body; when the vendor will not allow an unscripted camera; or when you need container-loading supervision at the GIDC gate. Name the agency, the AQL, and the hold-point on the PO. Intertek and TÜV regional inspectors also cover Gujarat—use whoever can be on the floor for your ship window, not the logo on a brochure.
After a remote pass, still require a physical first-article pack: samples from the production process, OES of that heat, gauge reports, and packing photos of the actual export carton. Remote audit qualifies the factory; FAI qualifies the lot.
7. Red Flags That Should Stop the Purchase Order
These are hold-or-exit conditions, not negotiating points. Document them on the scorecard and do not “watch the first shipment.”
- Tour confined to the office, showroom, or a single Swiss cell while cam capacity is “in another shed” you are not allowed to enter.
- OES, CMM, or salt-spray serial numbers that do not match equipment in the room; certificates from a lab the staff cannot walk you to.
- Alloy on the floor (or on bundle tags) different from the quoted grade, or scrap melt with no virgin-correction practice and no heat log.
- Refusal to title buyer-paid tooling, or samples run on a process that will not be used in production.
- No heat-number path from rod bundle to master carton; mixed lots in one inner box.
- Plating subcontracted to an unnamed job shop with no incoming micron check and no thread-offset rule.
- Blocks SGS, BV, or buyer video beyond a prepared corridor; ISO certificate that cannot be verified to the legal entity on the PI.
- Price that only works if MOQ, lead time, or Incoterms are left blank—then “clarified” after advance payment.
If two or more red flags appear, close the file and move to the next shortlisted unit. Jamnagar has enough turning capacity that you do not need to rehabilitate a factory that will not show process, lab, or title. Re-open only after written corrective action and a scored re-audit.
Frequently Asked Questions (FAQ)
Q: What weighted score should I require before awarding a production PO?
Use a 100-point scorecard. Require 75 or above, with no category below 3 out of 5, before a production PO. A lab score below 3 (rented certificates, no in-house OES or uncalibrated gauges) is an automatic hold even if the commercial quote is the lowest. Re-score after first-article and after any process or ownership change.
Q: How long does an on-site audit of a Jamnagar brass factory take?
A focused GIDC audit of a turning shop typically takes 3 to 5 hours: 45 minutes on rod/extrusion incoming, 90 minutes on cam versus Swiss CNC capacity and process control, 45 minutes in plating and packing, and 60 minutes in the quality lab reviewing OES prints, gauge calibration, CMM programs, and salt-spray records. Add a half day if you also walk a sister extrusion or foundry unit.
Q: Can a remote video audit replace walking the GIDC shop floor?
A live video walkthrough is enough to shortlist and to re-qualify a known vendor, but it should not replace a first-article on-site audit for a new production PO. Require unscripted camera movement through rod stores, machine bays, plating, packing, and the lab; match heat numbers on cartons to OES reports; and use SGS or Bureau Veritas when you cannot travel and the lot value or regulatory risk is high.
Q: Who should own brass tooling paid for by the buyer?
Cam form tools, Swiss collets, custom gauges, and plating jigs paid by the buyer should be titled to the buyer in the PO or a separate tooling agreement, with asset IDs, storage location, and a return clause. Factory-standard collets and worn inserts are consumables. Never leave ownership implied after a sample invoice.
Need an Auditable Jamnagar Brass Source?
Factories quoted through Jamnagar.net can be scored on shop-floor process, in-house lab evidence, and export packing—not catalogue PDFs alone.